- 2B / BW Shalimar Bagh, Opp. BQ Market, Near DLF Mall New Delhi - 110088, India.
- :+91-9312-871-070
Manufacturers, Exporters, Suppliers of Membrane Antiscalant
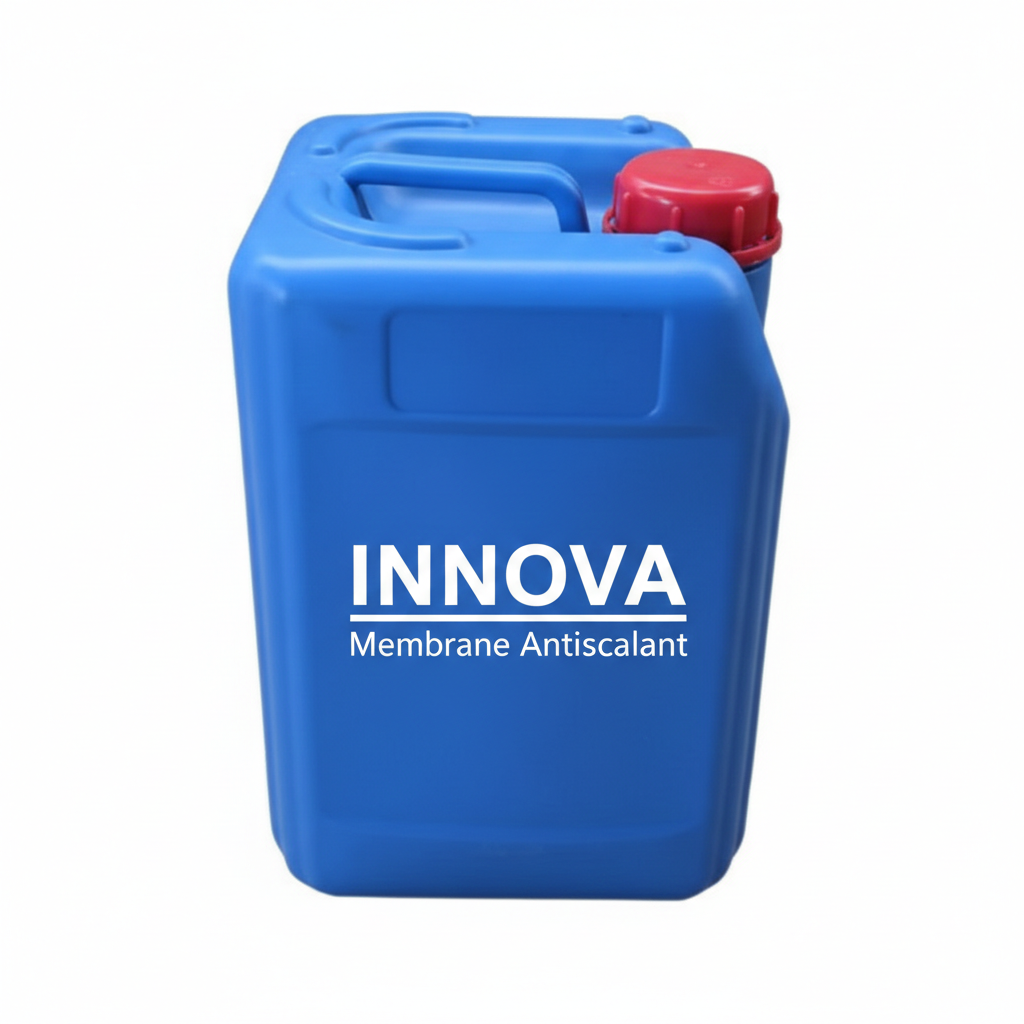
Universal RO Membrane Antiscalant & Antifoulant in USA
Innova Corporate (India) is a trusted manufacturer and supplier of high-grade Membrane Antiscalants in USA. American industrial water systems are more varied than most operators realize. Food processing plants in Colorado and Texas run on hard groundwater with elevated LSI. Pharmaceutical facilities in New England draw from clean but lightly mineralized sources where even modest hardness causes issues. Semiconductor fabrication plants in the Pacific Northwest and Mountain West need ultra-pure water with strict tolerances on dissolved solids. Southeast industrial facilities in Atlanta and Charlotte deal with a mix of surface and well water that shifts seasonally. Our universal membrane antiscalant is engineered to cover this full range, so plants across Denver, Seattle, Atlanta, Dallas and Boston get one product that handles the scale profile they actually face — without needing acid dosing or complex custom formulation.
Our RO Antiscalant in USA is a sophisticated super-threshold stabilizer designed to inhibit the precipitation of supersaturated salt solutions on membrane surfaces. By managing the nucleation and growth of crystals, it keeps scale precursors in solution even when the feed water is pushed past normal saturation limits. That eliminates the need for hazardous acid dosing, ensures a safer work environment, and achieves the highest possible plant conversion rates for systems operating at high recovery. For USA facilities running tight process water quality specs — particularly food, pharma and semiconductor plants — this combination of safety and performance is what makes the difference between stable long-term operation and unpredictable shutdowns.
The formulation provides comprehensive protection against a broad spectrum of foulants found in USA water sources, including Calcium Carbonate, Calcium Sulfate, Barium / Strontium / Magnesium Sulfates, Calcium Fluoride, Iron and Silica. This versatile chemical barrier keeps ions in suspension and prevents the scaling that leads to flux decline and high energy consumption. In facilities where membrane replacement costs run into hundreds of thousands of dollars, and where CIP downtime interrupts regulated production, getting this protection right is one of the highest ROI maintenance decisions the plant team can make.
Key Features & Strategic Benefits in USA:
- Enhanced System Recovery: Supports high recovery rates by maintaining clean membrane surfaces in USA food processing, pharmaceutical and industrial RO plants.
- Broad-Spectrum Control: Effective against the full range of mineral salts and metallic foulants that appear across American feed water sources.
- Low Dosage Efficiency: Highly concentrated formula that needs only minimal dosing, keeping operating cost low for USA industrial and municipal buyers.
- Phosphate-Free Performance: Unlike SHMP, it does not cause calcium or iron-based phosphate deposition in the membrane elements.
- Extended Cleaning Intervals: Noticeably reduces the frequency of membrane CIP cycles in USA, supporting uninterrupted production in regulated industries.
- Universal Compatibility: Safe for Polyamide, Thin-Film Composite and Cellulose Acetate membranes used across the country.
- Safe Handling: Non-hazardous and stable formulation that is easy to apply in USA industrial setups, with documentation formatted for FDA, EPA and state regulatory review.
Storage & Stability: To maintain product integrity for our USA clients, store in original containers in a cool, dry place. Keep away from heat sources and direct sunlight. For precise dosing calculations based on your USA feed water analysis, please consult our technical team and refer to the Material Safety Data Sheet (MSDS).