- 2B / BW Shalimar Bagh, Opp. BQ Market, Near DLF Mall New Delhi - 110088, India.
- :+91-9312-871-070
Manufacturers, Exporters, Suppliers of RO Antiscalant Chemicals
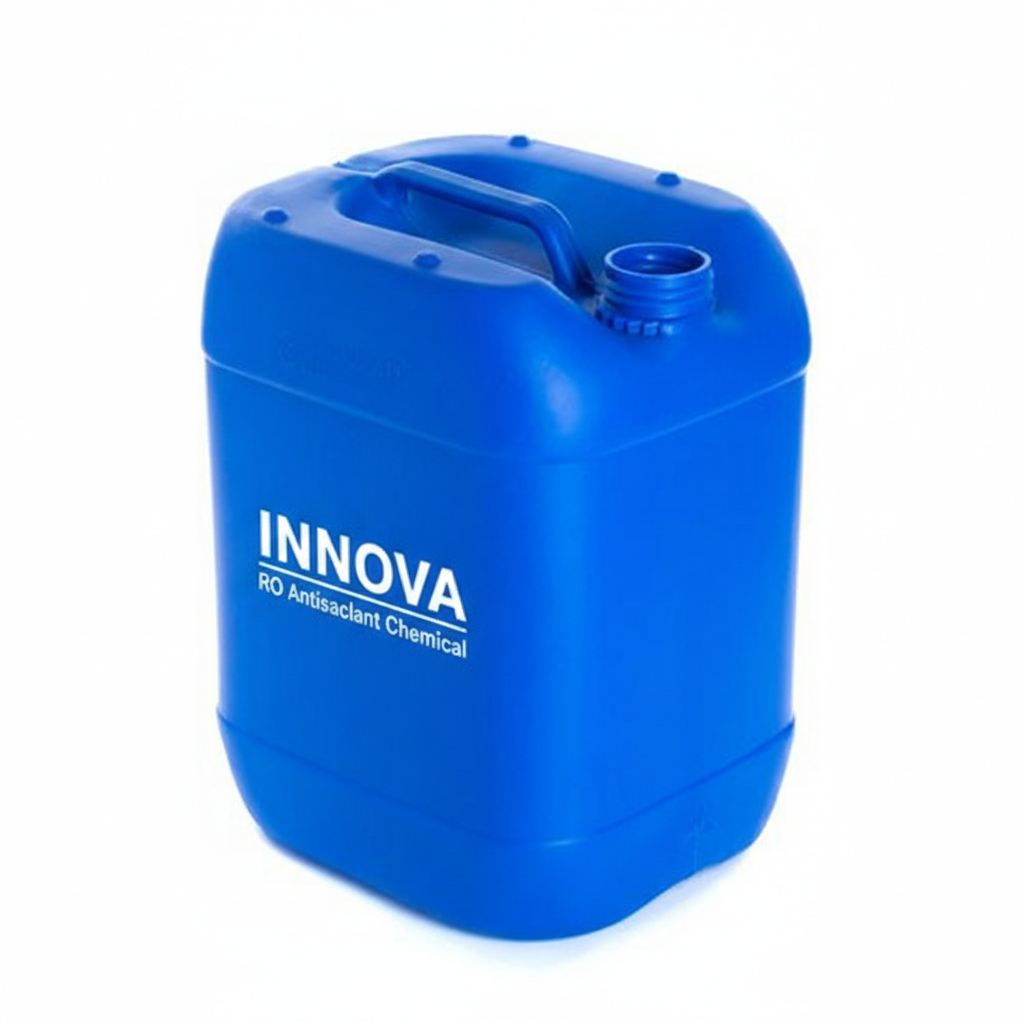
Industrial Grade RO Antiscalant & Antifoulant Chemicals in Maharashtra
Membrane scaling remains one of the most costly and persistent problems in industrial water treatment. When dissolved minerals in feed water concentrate beyond their solubility limits, they crystallise onto the membrane surface, forming hard deposits that choke productivity and drive up energy costs. Innova Corporate (India) has engineered a flagship RO Antiscalant Chemical in Maharashtra that functions as a protective barrier at the molecular level — interfering with crystal nucleation and growth before scale can ever take hold. This formulation represents the gold standard for membrane protection, trusted by industrial operators who cannot afford unplanned shutdowns or premature membrane replacement.
What distinguishes our antiscalant from conventional scale inhibitors is its threshold inhibition mechanism. Rather than removing hardness minerals from the feed stream through ion exchange or precipitation, the chemical works at sub-stoichiometric dosages to distort crystal lattice structures, keeping scale-forming compounds suspended in solution where they can be safely rejected. This approach allows businesses to maximise water recovery, reduce wastewater discharge volumes, and lower overall chemical consumption — outcomes that directly improve both environmental compliance and operating margins. For manufacturing plants that demand consistent, reliable protection across fluctuating feed water conditions, this product delivers performance that generic alternatives simply cannot match.
The formulation is equally effective across Reverse Osmosis (RO), Nanofiltration (NF), and Ultrafiltration (UF) systems, making it a versatile choice for diverse industrial applications — from brackish water treatment and seawater desalination pre-treatment to specialised high-recovery filtration trains where conventional antiscalants often fall short. Whether your plant operates on municipal supply, borewell water, or surface water sources with variable chemistry, our technical team can recommend the precise formulation to match your specific feed water profile.
Key Features & Strategic Advantages for Maharashtra Plants:
- Superior Scale Control: Effectively manages Calcium Carbonate up to LSI +3.0, along with Calcium Sulfate, Barium Sulfate, and Strontium Sulfate — the four most common scale-forming species in industrial feed waters.
- Softener Alternative: Delivers excellent results as a highly efficient, low-maintenance replacement for traditional softener filters, eliminating the need for salt regeneration, resin replacement, and the associated downtime.
- Potable Water Certified: Classified and safe for use in systems producing drinking water, meeting the regulatory requirements for municipal and community water supply applications.
- Wide Compatibility: Fully compatible with all leading RO membrane brands and downstream coagulants, allowing seamless integration into existing treatment trains without reformulation.
- Metallic Oxide Tolerance: Offers high tolerance to aluminium and iron oxides, preventing metallic fouling that is particularly common in groundwater sources with elevated dissolved metals.
- Operating Flexibility: Effective over a broad pH range and can be fed neat (concentrated) or diluted, giving operators flexibility in dosing system design and chemical storage.
- Particulate Dispersion: Acts as a powerful dispersant to keep silt, clay, and organic foulants from adhering to the membrane surface, complementing the antiscalant's crystal inhibition action.
At Innova Corporate, we understand that no two water sources are identical. That is why we offer a range of specialised R.O. antiscalant formulations tailored to specific water chemistries — from high-hardness groundwater and silica-laden surface water to brackish sources with elevated iron and manganese. Our technical team can assist you in selecting the precise formulation to ensure your system operates at peak recovery rates with minimal downtime. We also provide dosing calculations, compatibility testing, and on-site support to help you optimise chemical usage and achieve the lowest total cost of ownership for your membrane assets.