- 2B / BW Shalimar Bagh, Opp. BQ Market, Near DLF Mall New Delhi - 110088, India.
- :+91-9312-871-070
Manufacturers, Exporters, Suppliers of Membrane Antiscalant
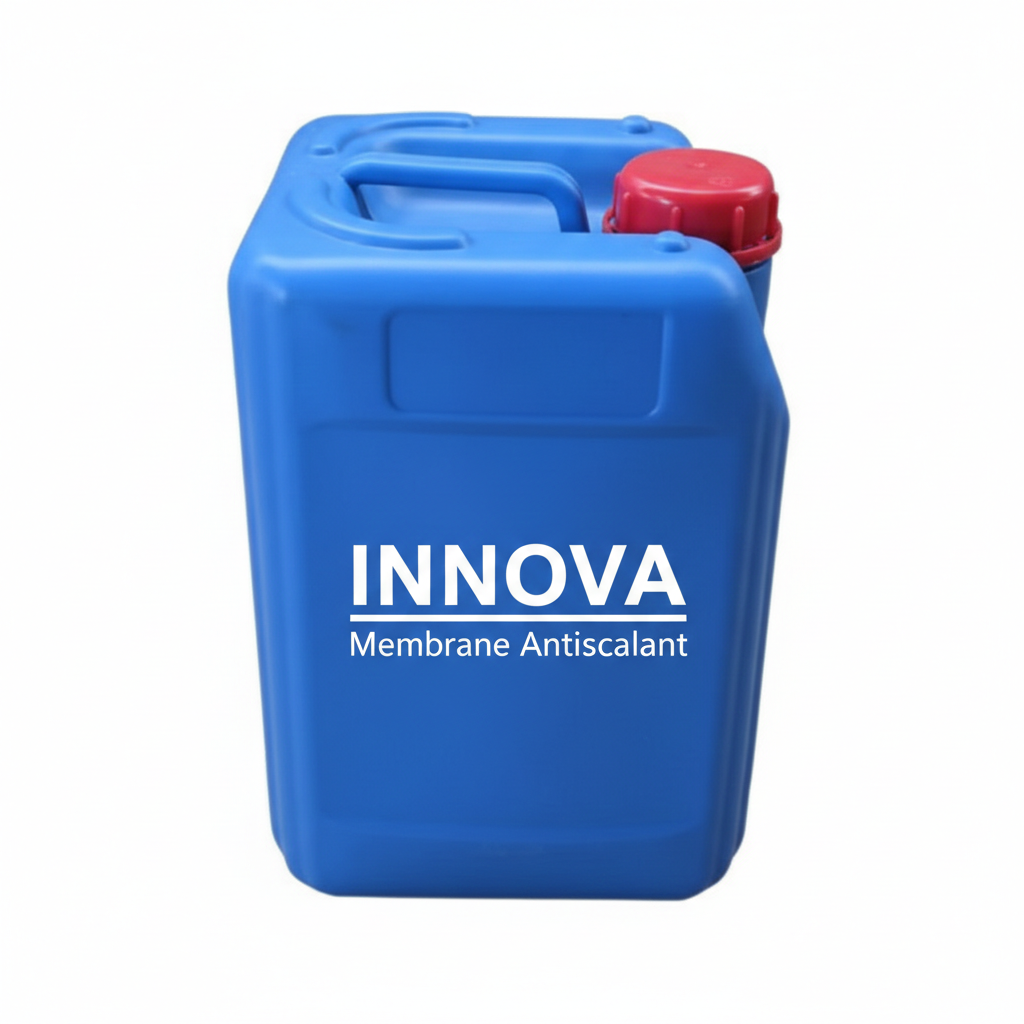
Universal RO Membrane Antiscalant & Antifoulant for High-Recovery Systems
Innova Corporate (India) is a leading manufacturer, bulk supplier, and global exporter of high-grade Membrane Antiscalants. From our production base in Delhi, we serve a wide network of clients throughout India while extending our supply chain to the Middle East, Africa, and Southeast Asia. Every batch is crafted using industrial-standard raw materials, delivering premium membrane protection at highly competitive market prices.
Our RO Antiscalant is a sophisticated super-threshold stabilizer engineered to inhibit the precipitation of supersaturated salt solutions on membrane surfaces. By managing the nucleation and growth of crystals, it eliminates the need for hazardous acid dosing — creating a safer work environment while achieving the highest possible plant conversion rates.
It delivers comprehensive protection against a broad spectrum of foulants, including Calcium Carbonate, Calcium Sulfate, Barium/Strontium/Magnesium Sulfates, Calcium Fluoride, Iron, and Silica. This versatile chemical barrier keeps ions suspended in the feed stream, preventing the scaling that leads to flux decline and elevated energy consumption.
Key Features & Strategic Benefits:
- Enhanced System Recovery: Supports high recovery rates by maintaining clean, scale-free membrane surfaces.
- Broad-Spectrum Scale Control: Effective against a wide range of mineral salts and metallic foulants including calcium, barium, strontium, iron, and silica.
- Low Dosage Efficiency: Highly concentrated formula requires minimal dosage (2–5 ppm), ensuring cost-effective operations.
- Phosphate-Free Performance: Unlike SHMP, it does not cause calcium or iron-based phosphate deposition on membranes.
- Extended Cleaning Intervals: Dramatically reduces the frequency of membrane CIP (Clean-in-Place) cycles by up to 50%, cutting downtime and labour cost.
- Universal Membrane Compatibility: Safe for use with all Polyamide, Thin-Film Composite (TFC), and Cellulose Acetate (CA) membranes.
- Hazard-Free Handling: Non-hazardous and chemically stable formulation for easy industrial application without special PPE beyond standard safety norms.
- Acid Dosing Eliminated: Replaces hazardous acid dosing, improving workplace safety and reducing chemical handling risks.
- Potable Water Compliant: Certified and safe for use in systems producing drinking water.
- Cost-Efficient Formulation: Premium performance at a competitive per-litre cost with a fast return on investment.
Technical Specifications
| Parameter | Value / Description |
|---|---|
| Product Type | Liquid RO Membrane Antiscalant & Antifoulant |
| Appearance | Clear to pale yellow, free-flowing liquid |
| Odour | Mild, characteristic — non-offensive |
| pH (1% solution) | 2.0 to 3.5 |
| Specific Gravity (at 25°C) | 1.10 to 1.25 |
| Water Solubility | Completely soluble in all proportions |
| Chemical Type | Phosphate-free, super-threshold stabilizer |
| LSI Tolerance | Up to +3.0 |
| Recommended Dosage | 2–5 ppm in RO feedwater (site-specific) |
| Foaming Tendency | Low — suitable for high-pressure RO systems |
| Storage Temperature | 5°C to 40°C — protect from direct sunlight |
| Shelf Life | 24 months from date of manufacturing |
| Packaging Options | 5L, 20L, 50L, 200L HDPE drums & IBC tanks |
At Innova Corporate, we recognise that every RO plant operates under unique water chemistry and process conditions. That is why we offer a diversified portfolio of Membrane Antiscalant grades — each formulated for specific salinity levels, temperature ranges, and recovery targets. Our Delhi-based technical specialists work closely with plant engineers to recommend the ideal formulation, ensuring peak recovery, stable flux, and long-term membrane protection.
Applications
| Industrial RO Plants | Textile, pharmaceutical, food processing, and power generation units |
| Brackish Water RO | High-TDS borewell, well water, and municipal supply treatment |
| High-Recovery Systems | RO plants operating above 75% recovery without scale issues |
| Multi-Foulant Water | Feedwater containing calcium, barium, strontium, iron, and silica |
| Commercial RO Systems | Hotels, hospitals, shopping malls, and residential complexes |
| ZLD & MEE Plants | Pre-treatment stage for Zero Liquid Discharge and MEE systems |
| Drinking Water Plants | Potable water RO plants for municipalities and communities |
| Cooling Tower Make-up | Scale control in cooling water circuits feeding RO systems |
Storage & Stability: To maintain product integrity, store in original sealed containers in a cool, dry place. Keep away from heat sources and direct sunlight. For precise dosing calculations based on your feedwater analysis, please consult our technical team and refer to the Material Safety Data Sheet (MSDS).
Why Choose Innova Corporate
| Manufacturing Expertise | In-house production with strict quality control at every stage |
| Global Export Network | Serving Middle East, Africa, and Southeast Asia with reliable logistics |
| Technical Support | Free dosing guidance and water analysis consultation from our Delhi team |
| Custom Formulations | Tailor-made antiscalant blends for unique water chemistry challenges |
| Bulk Supply Capability | Consistent stock availability for high-volume industrial buyers |
| Competitive Pricing | Factory-direct rates with transparent, no-hidden-cost invoicing |
Pricing & Supply
| Starting Price | From ₹480 per litre (bulk order slabs apply) |
| Custom Pricing | Special rates for 200L+ drums, IBC tanks, and export consignments |
| Minimum Order Quantity | 20 litres (sample quantities available on request) |
| Delivery Timeline | Pan-India dispatch within 3–5 working days |
| Payment Terms | Flexible options for regular and export buyers |
| Export Packaging | UN-approved HDPE drums & IBC totes for international shipping |
Dosing & Handling Guidelines
| Dosing Point | Injected into RO feedwater upstream of the cartridge filter |
| Dilution | Can be dosed neat or diluted with demineralised water |
| Dosing Equipment | Standard chemical dosing pumps (PP/PVDF wetted parts) |
| Handling Safety | Use gloves and eye protection; avoid skin contact |
| Storage | Store in a cool, dry, ventilated area away from direct sun |
Frequently Asked Questions (FAQ)
| Q1. What is a Membrane Antiscalant? | A Membrane Antiscalant is a specialised liquid chemical dosed into RO feedwater to prevent mineral salts — such as calcium carbonate, calcium sulfate, barium sulfate, strontium sulfate, and silica — from precipitating and forming scale on reverse osmosis membrane surfaces. |
| Q2. How does Membrane Antiscalant extend RO membrane life? | By keeping scale-forming minerals suspended in the feed stream, Membrane Antiscalant prevents crystallisation on the membrane. This reduces chemical cleaning frequency, maintains stable flux and rejection rates, and adds years to the operational life of RO membrane elements. |
| Q3. What is the recommended dosage of Membrane Antiscalant? | The typical dosage ranges from 2 to 5 ppm in RO feedwater, depending on feedwater analysis, LSI value, recovery rate, and membrane type. Free site-specific dosing guidance is provided by our technical team. |
| Q4. Which scales does Membrane Antiscalant control? | Our Membrane Antiscalant effectively controls calcium carbonate, calcium sulfate, barium sulfate, strontium sulfate, calcium fluoride, iron, silica, and metal oxide scales commonly found in industrial RO systems. |
| Q5. Is Membrane Antiscalant safe for drinking water plants? | Yes. Our Membrane Antiscalant formulation is certified and classified as safe for use in systems producing potable or drinking water, complying with industry-recognised health and safety standards. |
| Q6. Can Membrane Antiscalant replace a water softener? | Yes. Our Membrane Antiscalant acts as a highly efficient, low-maintenance alternative to traditional softener filters. It eliminates the need for regeneration salt, brine discharge, and frequent resin replacement. |
| Q7. Which RO membranes are compatible with this antiscalant? | Our Membrane Antiscalant is fully compatible with Polyamide, Thin-Film Composite (TFC), and Cellulose Acetate (CA) membranes, including all leading brands such as Dow FilmTec, Hydranautics, Toray, and LG. |
| Q8. What is the LSI tolerance of Membrane Antiscalant? | Our formulation effectively controls calcium carbonate scale at LSI values up to +3.0, making it suitable for high-recovery and high-hardness water applications. |
| Q9. What is the shelf life of Membrane Antiscalant? | The product has a shelf life of 24 months from the date of manufacturing when stored in its original sealed container at temperatures between 5°C and 40°C, away from direct sunlight. |
| Q10. In what packaging sizes is Membrane Antiscalant available? | We supply Membrane Antiscalant in 5L, 20L, 50L, and 200L HDPE drums, along with IBC tanks for bulk industrial requirements. Custom packaging is available for export orders. |
| Q11. How is Membrane Antiscalant dosed into the RO system? | It is injected into the RO feedwater upstream of the cartridge filter using a standard chemical dosing pump with PP or PVDF wetted parts. It can be dosed neat or pre-diluted with demineralised water. |
| Q12. Do you supply Membrane Antiscalant outside India? | Yes. We supply Membrane Antiscalant across India and export to the Middle East, Africa, and Southeast Asia with UN-approved export packaging and reliable logistics support. |